


Last Updated
Key Takeaways
Generated from the text of customer reviews
SafetyChain is a digital plant management and quality platform for food and beverage manufacturers. Quality, production, FSQA, and supplier teams use it across plant operations. Reviews praise its ease of use, flexibility, and support, while integration and enterprise management draw some criticism. In July 2026, SafetyChain expanded CAPA with reporting and supplier collaboration capabilities.
Our Verdict
SafetyChain is a strong option for food and beverage manufacturers with established quality and compliance operations, particularly those managing multiple teams or facilities. Its breadth suits organizations moving beyond manual processes. Facility-based pricing and custom quotes can make upfront cost comparisons difficult. We recommend it for manufacturers seeking a long-term platform for plant-wide quality management.
Overall Rating
Based on 20 users reviews
4.4
Rating Distribution
Positive
95%
Neutral
5%
Negative
0%
Starting Price
Custom Pricing
SafetyChain Specifications
- Incident Management
- Safety Management
- Dashboards
- Mobile Access
What Is SafetyChain?
SafetyChain is a food safety, quality, and operations management platform built for manufacturing plants. It offers digital forms, workflows, and real-time data that can replace paper records, spreadsheets, and disconnected tools. Using the software, teams can manage inspections, audits, SOPs, HACCP monitoring, GMPs, sanitation programs, CAPA workflows, and other food safety processes from one system.
Its configurable workflows can be deployed across locations, while integrations support existing technology environments. The platform also connects quality, compliance, production, and supplier processes to improve plant operations.
What Is SafetyChain Best For?
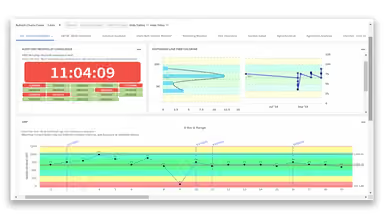
Among the different SafetyChain features, it stands out for 'Production Performance'. This feature connects live production data with the quality signals behind performance changes. It provides real-time visibility into throughput, downtime, yield, and scrap alongside in-process checks and SPC trends. Using this feature, teams can spot production drift early, assign corrective actions, and verify that issues are resolved before they lead to greater waste or downtime. This makes SafetyChain well suited for food manufacturers needing to monitor production performance and address quality-related losses while runs are still underway.
How Much Does SafetyChain Cost?
SafetyChain price is estimated to start at $150/month for a small business with 1 user. A large organization can expect to pay somewhere between $8,000-$25,000/month. The vendor offers three different plans as well, all available on custom pricing. These include:
- Essentials
- Advanced
- Supplier
Besides the base subscription cost, organizations should also factor in the following potential additional expenses:
- One-Time Implementation/Setup Fee: $18,000–$22,000, scales with number of on-site visits and package complexity
- Hardware Devices: $400–$800/device, sourced separately by the buyer
- IoT Data And Ignition Module Add-On: $600–$1,000/month/facility for real-time machine data streaming
- Sandbox Training Environment: $300–$500/month, optional
- Custom ERP/MES/SCADA Integration: $5,000–$15,000 one-time, varies by source system complexity
Disclaimer: Pricing references are based on publicly available third-party information and industry benchmarks. Actual costs may vary.
SafetyChain Integrations
The vendor hasn’t provided details about SafetyChain's integration with third-party apps.
How Does SafetyChain Work?
Follow the steps outlined below to get started with SafetyChain after you have logged in:
- Set up digital forms to replace paper-based checklists for GMPs, HACCP, sanitation, and pre-op inspections
- Configure supplier programs to collect certifications, specifications, and compliance documentation from vendors
- Capture plant floor data by having operators log inspection results, sensor readings, and production checks directly on tablets or mobile devices
- Track deviations by flagging out-of-spec results as they occur, so quality teams can respond before issues move downstream
- Manage corrective actions by assigning ownership, documenting root cause, and recording verification steps through to closure
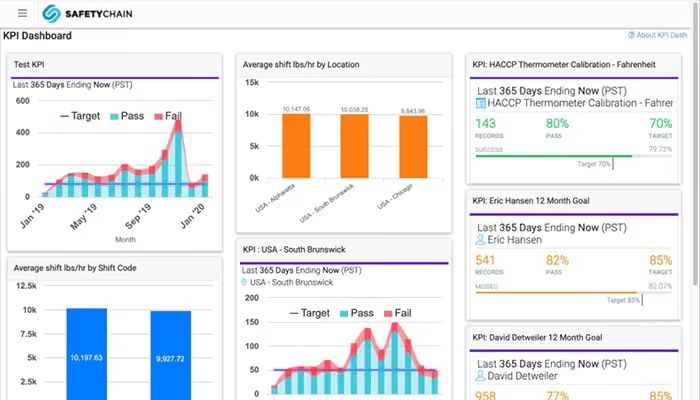
- Monitor operations through dashboards that show program status, open issues, and trends across lines, shifts, and facilities
- Generate audit-ready records by storing timestamps, signoffs, and corrective action history in one centralized system
- Review reports across multiple sites to compare performance and identify recurring quality or compliance patterns
Who Is SafetyChain For?
The platform suits different businesses operating across different industries and sectors. These include:
- Poultry
- Food and beverage
- CPG
- Packaging
SafetyChain Use Cases
Based on our analysis of SafetyChain features and user reviews, we have identified the following key business scenarios where it is well suited:
FSQA Teams Preparing For Food Safety Audits
FSQA teams can use SafetyChain when they need to maintain accessible records for internal and external audits. The platform fits operations that need to maintain programs such as HACCP, GMP, sanitation, and facility audits without relying on scattered paper records. It is especially relevant for plants that need to retrieve documented evidence quickly during regulatory, certification, or customer audits.
Multi-Plant Quality Teams Standardizing Food Safety Processes
SafetyChain can be used by corporate quality teams overseeing several facilities to establish consistent processes across locations. This scenario fits manufacturers that need the same quality checks, food safety programs, and corrective-action practices followed across multiple plants. It offers centralized visibility that gives leadership a way to compare issues and trends across facilities rather than managing each site as a separate system. Users particularly appreciate how it makes it easier to collect data from different sources or sites.
Production Teams Addressing Yield And Process Variability
Production and quality teams can use SafetyChain when changes in yield, scrap, downtime, or throughput need to be connected to the quality conditions behind them. This is useful for plants where small process deviations can lead to overpack, rework, waste, or production losses during a run. When managers have access to production performance and quality signals, they are better positioned to investigate problems while production is still underway. This way, they can standardize how deviations are corrected.
Supplier Quality Teams Managing Incoming Materials And Certifications
SafetyChain supports supplier quality teams when they manage compliance documentation and incoming inspections across a large supplier base. The scenario is particularly relevant for manufacturers that need to track certificates, receive checks, and supplier issues. It also helps them take corrective actions before materials affect production. Connecting supplier status with receiving and quality workflows provides a clearer way to identify supplier-related risks across plants.
Is SafetyChain Right For You?
SafetyChain is best suited to established food and beverage manufacturers with quality and compliance processes across one or more facilities. Its configurable setup can support different procedures by plant, product, or program. It also works with existing ERP, MES, equipment, and other plant systems. This makes it a better fit for companies that want to build on their current technology.
Security is an important consideration for manufacturers handling operational and compliance data. SafetyChain uses encrypted data, role-based permissions, and private cloud tenancy to protect customer information. The company also announced its SOC 2 Type 2 certification in February 2026. The certification covers controls for security, availability, and confidentiality.
SafetyChain lists Tyson Foods, Albertsons Companies, Blue Bell, Butterball, Driscoll’s, Home Chef, Schwan’s Company, See’s Candies, Trident Seafoods, and White Castle among its customers. The company has also addressed FSMA 204 in its recent industry guidance. Its January 2026 content discusses food traceability readiness, while its June 2026 guidance examines FSMA 204 alongside 21 CFR Part 117. The platform supports related processes such as receiving inspections, supplier compliance, pre-shipment reviews, and food safety record management.
Still doubtful if SafetyChain is the right fit for you? Connect with us at (661) 384-7070 for further guidance.
SafetyChain Features
In-Process Quality
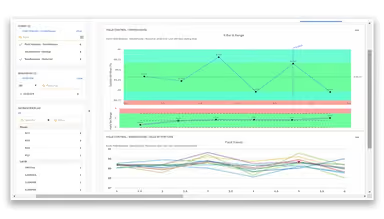
SafetyChain helps food manufacturers monitor product quality while production is underway. Teams can capture measurements, track SPC trends, and respond to deviations before they lead to waste, rework, or nonconforming products. At the same time, operators and quality teams can also manage alerts, corrective actions, product holds, and verification within the production workflow.
Food Safety Programs
The platform brings key food safety programs into a single digital workflow. Such a program covers areas such as Pre-Op inspections, GMPs, sanitation, facility audits, receiving inspections, and HACCP monitoring. Using this feature, teams can assign checks, flag deviations, and track corrective actions through verification and closure. Standardized workflows can also be applied across plants and shifts, giving quality and plant teams a consistent way to manage food safety execution.
CAPA Management
This feature gives food and beverage teams a structured way to investigate non-conformances and follow each issue through to resolution. CAPAs can be linked to inspections, audits, CCP checks, complaints, and supporting records. This helps keep the related evidence together. QA, production, maintenance, and sanitation teams can work from assigned tasks and deadlines, while dashboards provide visibility into CAPA status across facilities.
Process And Data Controls
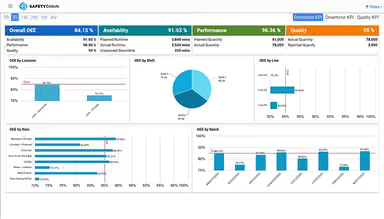
SafetyChain puts live production data closer to the people making decisions on the plant floor. It enables operators and quality teams to monitor process variation, weight checks, and other measurements as production runs. Its dashboards surface trends by line, shift, or SKU. SafetyChain can also connect ERP, MES, WMS, and plant-floor data, giving teams a more complete view of process performance.
Pros And Cons of SafetyChain
Pros
Forms are somehow easy to use for data collection
Users appreciate the platform’s customization options
Reviewers value access to real-time quality and production data
Many users find it supports multiple food safety processes
Reviewers find it adaptable to different manufacturing needs
Cons
Managing large enterprises may require multiple integrations
Some reviewers find the reporting tools limited
Users note gaps in document management
SafetyChain Pricing
Essentials | Advanced | Supplier |
|---|---|---|
Custom Pricing | Custom Pricing | Custom Pricing |
|
|
|
Disclaimer: The pricing details were last updated on Sep 25, 2026 from the vendor's website. Please contact us for a tailored pricing list.
SafetyChain Reviews
Total 20 reviews
4.4
All reviews are from verified customers
Rating Distribution
5
Stars45%
4
Stars50%
3
Stars5%
2
Stars0%
1
Stars0%
Share your experience
Food Production, 51-100 employees
More than a year
“Very flexible and helpful”
Pros
I love how easy it is to build reports and dashboards. With just one click, different departments can access the data they need without any hassle.
Cons
Creating a new product takes a lot of time, especially when I have to manually add it to every single form.
Rating Distribution
Ease of use
10
Value for money
10
Customer Support
10
Functionality
10
Apparel and Fashion, 1-10 employees
Less than 6 months
“Take it slow when starting with this software”
Pros
The structured workflow makes daily tasks so much more manageable. It clearly shows the time needed to complete them and flags any overdue statuses, keeping everything on track.
Cons
I have run into multiple login issues and the occasional system crash, which can be frustrating, especially when I am in the middle of something important.
Rating Distribution
Ease of use
6
Value for money
6
Customer Support
6
Functionality
6
Architecture and Planning, 500+ employees
More than a year
“Dedicated to ensuring food safety”
Pros
I have been using this software since its early days and the experience has been both rewarding and enjoyable. SafetyChain has remained committed to creating a user-friendly food safety solution. Form development is simple and using the app is just as easy.
Cons
The app uses a lot of bandwidth so when I am in a spot with weak Wi-Fi, I have to rely on offline mode more than I would like.
Rating Distribution
Ease of use
9
Value for money
10
Customer Support
10
Functionality
10
Frequently Asked Questions
Does SafetyChain offer an API?
Yes, it offers API access.
What language does SafetyChain support?
SafetyChain software is available in English language.
What other apps does SafetyChain integrate with?
The vendor hasn't provided details about the platform's third-party integrations.
Does SafetyChain have a mobile app?
Yes, it offers a mobile app for Android and iOS devices.
What types of pricing plans does SafetyChain offer?
With an expected starting price of $150/month for small businesses, the vendor offers multiple custom priced pricing plans. These include Essentials, Advanced, and Supplier. Get a tailored SafetyChain cost estimate.
Who are the typical users of SafetyChain?
The platform is used by poultry, packaging, CPG, and food and beverage businesses.
What level of support does SafetyChain offer?
The vendor offers support via phone, email, SafetyChain University, and help center.